

Discover top-tier automated chicken harvesting robotics and bio-shielded poultry logistics systems engineered for commercial agribusiness integrators.
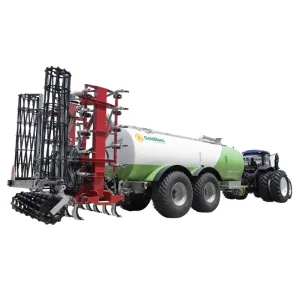
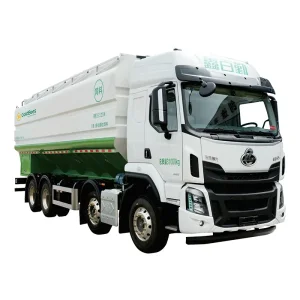
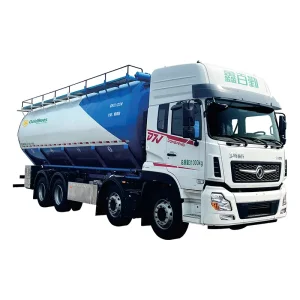
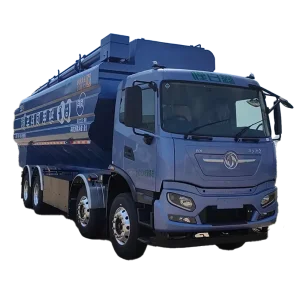
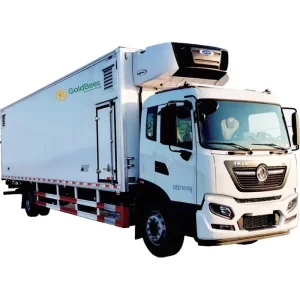

Overcoming global agricultural labor shortages, elevating bird welfare standards, and mitigating biosecurity contamination vectors in commercial broiler production.
The commercial poultry harvesting industry is undergoing an unprecedented operational paradigm shift. For decades, the broiler loading phase has relied almost exclusively on intensive manual catching crews working in hazardous, dust-choked, low-light environments. Modern mega-integrators and industrial meat processing enterprises now face crippling chronic labor deficits, soaring hourly turnover rates, and stringent regulatory penalties surrounding animal welfare. Identifying and deploying the best chicken catching robot suppliers and products has shifted from an optional efficiency optimization to an existential supply-chain mandate.
Robotic chicken harvesting eliminates human physical variability while enforcing continuous operating velocity. By pairing automated poultry gatherers with integrated bulk feed haulage and specialized climate-regulated transport vehicles, industrial broiler operations achieve complete traceability, eliminate biosecurity breaches, and drastically lower bird stress, bruising, and DOA (Dead on Arrival) ratios.
Manual catching frequently inflicts acute wing fractures, hematomas, and internal bleeding. Robotic harvesters incorporate gentle polyurethane rotating fingers and variable-speed contour conveyors, slashing carcass downgrade penalties at the slaughterhouse by up to 68%.
Catching crews travelling across multiple independent farms act as primary super-spreaders for avian influenza and pathogens. Robotic platforms remain dedicated to designated biosecure zones, built with sealed electronics capable of withstand 80°C chemical washdowns.
Manual crews operate on volatile schedules plagued by high absenteeism and ergonomic strain. Robotic systems deliver fixed-rate handling capacities of 6,000 to 9,000 birds per hour, synchronizing farm pickup seamlessly with processing line intake slots.
Inside the engineering mechanics: How computer vision, soft-contact robotics, and automated crate transfer establish operational supremacy.
A world-class intelligent chicken harvester integrates specialized multi-disciplinary engineering adapted to demanding poultry house atmospheres characterized by high ammonia concentrations, airborne feather dander, and deep litter topography.
| Engineering Attribute | Manual Catching Crews | Gen-2 Mechanical Harvesters | Intelligent AI Catching Robots |
|---|---|---|---|
| Throughput (Birds/Hr) | 3,000 – 4,500 (Fatigues) | 5,000 – 6,500 | 8,000 – 10,000 (Constant) |
| Carcass Downgrades | 3.5% – 6.0% | 1.8% – 2.5% | < 0.8% Certified |
| Biosecurity Risk | Extreme (Human vector) | Moderate (Complex wash) | Zero (Dedicated IP69K unit) |
| House Environmental Impact | High (Open doors, dust) | Medium (Exhaust fumes) | Clean (Electric/Hybrid drive) |
Leveraging vertically integrated manufacturing excellence, deep agricultural engineering heritage, and precision fabrication campuses.
Xinbaiqin Special Vehicle Co., Ltd. operates a high-capacity manufacturing facility in Cixi, Zhejiang. Encompassing robotic laser welding, CNC bending cells, surface phosphating, and electrostatic powder coating, every structural chassis and specialized body is forged completely in-house.
Operating in strategic electromechanical partnership with CP M&E, GoldBees platforms are field-tested within the world's most demanding vertically integrated broiler systems. We solve live farming problems with field-tested durability, not theoretical bench prototypes.
Unlike standalone vehicle builders or niche robot shops, GoldBees provides complete farm-to-processing integration: feed transportation (auger & pneumatic), live broiler loading machinery, and multi-tier insulated transport trailers equipped with microclimate telemetry.
Key technical checkpoints required by poultry processing conglomerates, corporate integrators, and international logistics directors.
Global fleets demand chassis flexibility. GoldBees vehicles configure seamlessly with leading international platforms—including Scania, Volvo, MAN, Isuzu, and Sinotruk—guaranteeing localized serviceability.
Frequent disinfection using chlorinated and quaternary ammonium agents degrades standard automotive electronics. Our harnesses feature molded IP69K connectors, fluoropolymer insulation, and aircraft-grade aluminum bodies.
Modern integrators demand real-time transparency. Every system can interface via CAN-bus to cloud telemetry, monitoring compartment temperatures, CO2 levels, unloading speeds, and robotic operational uptime.
Full international certification documentation including CE machinery safety directives, electrical EMC standards, and national weight/axle distributions are provided for turnkey homologation across export markets.
Connect robotic catching efficiency directly into high-payload feed transport and biosecure logistics infrastructure.

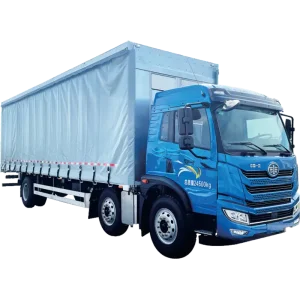

Ensuring zero operational downtime across 6 continents through factory-certified engineering support, spare parts availability, and strict adherence to international transport mandates.
Factory-trained engineers provide on-site calibration, operator staff training, and house-entry adaptation anywhere globally. Complete digital twin simulators ensure crew readiness prior to equipment arrival.
Centralized inventory hubs in Asia, Europe, and the Americas keep essential hydraulic valves, soft-catch elastomer fingers, PLC controllers, and optical sensors ready for emergency dispatch.
We supply complete engineering calculation records, including brake distribution analysis, axle weight simulations, and electrical safety certificates, ensuring seamless customs clearance and road registry approval.
Key operational questions addressed by our chief robotics and special vehicle engineering teams.