Explore field-tested transport platforms and agro-industrial solutions engineered to protect high-value genetics, reduce mortality, and elevate transit biosecurity.
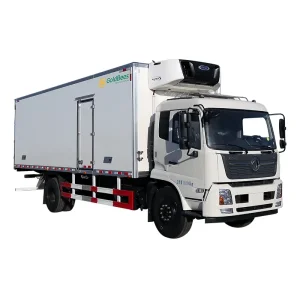
China China Suppliers Goldbees Refrigerated Cold-Chain Transport Truck - Intelligent Multi-Functional Solutions from Factory Factories, Product
View Specifications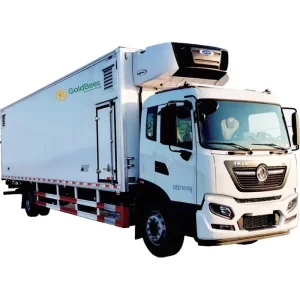
Best China Suppliers GoldBees Fully Enclosed Automated Day-Old Chick Transport Truck from Factory - Precision Livestock Logistics Factories, Products
View Specifications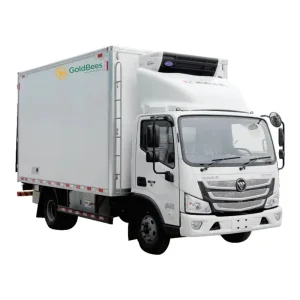
Custom China Fresh Produce Sorting & Transport Vehicle - Efficient, High-Capacity Solution from Top Suppliers & Factory Factory, Products
View Specifications
Famous China GoldBees Livestock Transport Semi-Trailer: Leading Suppliers and Factory for Safe Pig Transportation Supplier, Company
View Specifications
Custom China Suppliers and Factory of CP M&E Poultry, Livestock Farming & Feed Mill Equipment for Sustainable Meat Industry Manufacturer, Product
View Specifications
Famous China M&E Suppliers: Advanced Poultry & Livestock Farming Equipment for Feed Mills and Food Factories Supplier, Company
View Specifications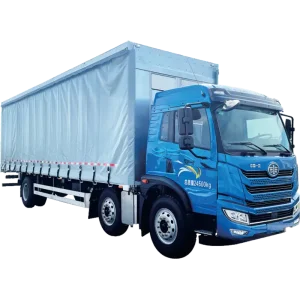
ODM China Suppliers GoldBees Broiler Transport Truck - Safety, Comfort, and Durability for Poultry Transit Factory Supplier, Factory
View Specifications
ODM China GoldBees Livestock Transport Truck - Safe Solutions from Leading Suppliers and Factory for Pig Transportation Supplier, Product
View SpecificationsWhy modern hatcheries and industrial poultry integrators cannot treat day-old chick (DOC) shipping as standard cold-chain trucking.
In modern commercial poultry operations, the transit phase represents one of the most critical threats to lifetime flock performance. Day-old chicks (DOC) are biologically poikilothermic—meaning they lack autonomous thermoregulatory control during the first 72 to 96 hours of post-hatch life. Unlike adult birds or static freight, newborn chicks rely entirely on their ambient microenvironment to maintain an internal rectal core temperature between 40.0°C and 40.5°C (104°F to 105°F).
Deviation from this thermal comfort band triggers devastating physiological consequences. When cargo compartment temperatures plunge below 30°C without adequate insulation and airflow dampening, chicks huddle together to conserve heat, leading to mechanical suffocation and progressive hypothermia. Conversely, when internal temperatures climb above 35°C combined with elevated metabolic relative humidity, neonatal birds experience rapid dehydration, irreversible organ stress, and accelerated yolk sac resorption failure. Empirical field evaluations demonstrate that transit-induced stress increases early 7-day mortality by up to 3.5%, deteriorates life-cycle Feed Conversion Ratios (FCR) by 4 to 8 points, and permanently impairs intestinal villi development.
Consequently, procurement executives and fleet directors at global breeding operations—including Cobb-Vantress, Aviagen, and CP Group subsidiaries—now prioritize dedicated, climate-automated day-old chick transport trucks over generic insulated dry vans.
Global poultry consumption demands moving between 50,000 and 150,000 live chicks per vehicle per delivery cycle. At these packing densities, the collective metabolic heat production of chicks generates up to 12 to 15 Watts per kilogram, creating a severe internal heat island without high-volume forced laminar air distribution.
Transboundary animal diseases, specifically Highly Pathogenic Avian Influenza (HPAI) clades and virulent Newcastle Disease, have made vehicles the primary vector of cross-facility contamination. Modern day-old chick transport requires absolute microbial barrier engineering.
Fleet operators demand optimized payload capacities achieved through high-strength aeronautical aluminium chassis integration. Lightened vehicle tare weight directly converts into legal payload headroom, decreasing fuel consumption per delivered bird.
The core technological differentials that distinguish GoldBees / Xinbaiqin engineering from conventional truck bodybuilders.
Conventional reefer units blast cold air across the ceiling, expecting it to filter passively down through densely stacked chick crates. This inevitably creates extreme temperature stratification: freezing conditions in the top crates and suffocating, lethal hot spots in the center and bottom decks. GoldBees by Xinbaiqin deploys an engineered Underfloor Forced-Laminar Positive-Displacement Air Channel System.
Conditioned, fresh, and filtered air is channeled through pressurized floor plenums and forced vertically through precision-perforated chick box corridors. This guarantees that every single chick crate—from the bulk-head front to the rear hydraulic tail-lift—experiences uniform air velocity (0.3 to 0.5 m/s) and exact thermal parity (tolerance within ±0.5°C across the entire 13.6-meter trailer box).
Autonomous infrared gas sensors continuously monitor ambient CO₂ concentrations. If levels exceed 1,500 ppm, exhaust louvers automatically trigger 100% fresh-air purge cycles within 45 seconds without destabilizing box temperature.
To eliminate single-point mechanical failure in transcontinental transit, our systems pair the truck PTO with an independent, sound-insulated water-cooled diesel auxiliary generator delivering uninterrupted HVAC runtime.
Seamless food-grade antibacterial gel-coated fiberglass reinforced panels (FRP) with rounded internal sanitary coves. Devoid of structural rivets or unsealed crevices, enabling rapid terminal chemical foam sanitation.
Real-time IoT cloud connectivity streaming crate-level temperature, static duct pressure, humidity, fuel telemetry, and door open/close logs directly to hatchery command centers with instant SMS alarm triggers.
Engineered to perform in the planet's most grueling transport environments, from scorching desert routes to remote highland gravel roads.
Challenge: Ambient temperatures frequently exceed +48°C (118°F) combined with severe fine-dust sandstorms and long highway travel legs between nucleus breeding centers and desert growing sheds.
Engineered Solution: High-ambient tropicalized multi-stage condenser configurations, dual centrifugal dust pre-filters before HEPA air intakes, and ultra-dense 85mm polyurethane vacuum-bonded insulation walls.
Challenge: Year-round 85% to 95% relative humidity combined with sudden monsoon downpours and dense urban congestion that restricts vehicle airflow.
Engineered Solution: Active refrigeration dehumidification coils integrated with modulated electric reheating cores. System strips moisture from fresh air before circulating it, preventing wet chick down and fungal spore proliferation.
Challenge: Sub-zero winter operations falling to -35°C (-31°F) with high road chemical de-icing salt exposure and risks of cargo hypothermia during loading/unloading.
Engineered Solution: High-output independent diesel hydronic heating matrices with heat-recovery ventilation (HRV) units. Anti-corrosive galvanized and stainless steel sub-frames engineered for harsh winter conditions.
A manufacturing partnership bridging automotive coachbuilding excellence with global agribusiness experience.
What establishes Xinbaiqin Special Vehicle Co., Ltd. as an elite supplier in live animal logistics is its intrinsic relationship with CP M&E, the specialized electromechanical arm of Charoen Pokphand Group. Unlike generic vehicle modification factories that assemble bodies from off-the-shelf catalog drawings, our engineering originates directly from daily feedback loops across CP Group’s vast network of commercial hatcheries, feed mills, and parent stock farms.
Our 66,667 m² manufacturing headquarters located in Cixi, Zhejiang Province, China operates high-precision robotic laser cutting stations, automated panel foaming presses, and dedicated climate-chamber test laboratories. We do not merely manufacture a shell; we engineer the entire biological ecosystem including hydraulic floor lifts, positive-pressure air delivery ducting, auxiliary energy powerplants, and washdown-safe electrical controls.
Our transport superstructures seamlessly mount onto major global commercial chassis platforms including Scania, Volvo, Mercedes-Benz Actros, MAN, FAW, Foton, and Sinotruk, ensuring compliance with local gross vehicle weight ratings (GVWR) and axle layout regulations.
Every GoldBees production line adheres to stringent ISO 9001 quality management, CE electrical certification, and ATP international sanitary transportation standards, accompanied by full English export documentation and type-approval support.
Beyond mobile transport units, we collaborate across CP M&E’s engineering division to provide integrated EPC solutions encompassing modern feed milling, smart climate-controlled breeder housing, and fully automated processing lines.
Anticipating the technological transformation of animal protein logistics through electrification, edge AI, and autonomous handling.
In response to stringent corporate ESG mandates and zero-tailpipe-emission municipal zones, Xinbaiqin has engineered China's first commercial New Energy Vehicle (NEV) poultry haulers. Featuring lithium iron phosphate (LFP) high-density battery architectures and 800V silicon-carbide inverter drives, these units power microclimate HVAC systems cleanly and silently, eliminating exhaust ingestion near clean hatchery docks.
Transitioning from reactive thermostats to neural-network predictive microclimate models. By integrating real-time weather forecasting, road slope topography, and bird age/weight metrics, our onboard AI system preemptively modulates blower CFM outputs and thermal injection 15 minutes before the truck encounters high mountain passes or severe ambient heat waves.
To eliminate manual labor, ergonomic injuries, and loading dock biosecurity breaches, the 2026 GoldBees platform introduces standardized automatic robotic arm docking. Complete dollies of 120 chick boxes are ingested, locked, and weight-balanced within 8 minutes via automated guided roller decks.
Essential considerations for fleet directors, hatchery managers, and international equipment buyers.
Complete the poultry and livestock value chain with specialized bulk auger trucks, cold chain distribution semi-trailers, and automated farm equipment.

Best Goldbees Refrigerated Cold-chain Transport Semi-trailer---Intelligent Multi-Functional Transportation Manufacturers, Companies
View Specifications
High-Quality China GoldBees Refrigerated Cold-Chain Transport Semi-Trailer - Reliable Suppliers & Advanced Factory Solutions Manufacturers, Factories
View Specifications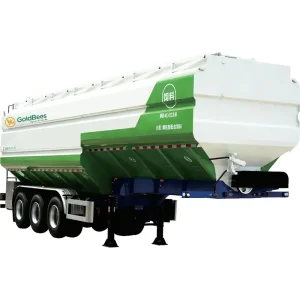
Best China GoldBees Electric/Hydraulic Auger Conveyor Semi-Trailer - High Efficiency & Durability from Trusted Suppliers and Factory Manufacturer, Company
View Specifications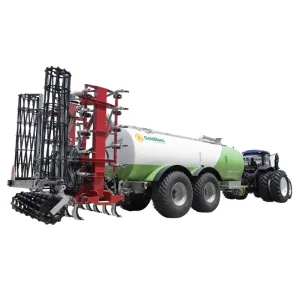
China Transform your poultry operations with intelligent automation—where speed, accuracy, and animal welfare converge Factory, Product
View Specifications
High-Quality China Suppliers of Poultry and Livestock Farming Equipment | Complete Feed Mill Factory Solutions Manufacturers, Manufacturer
View Specifications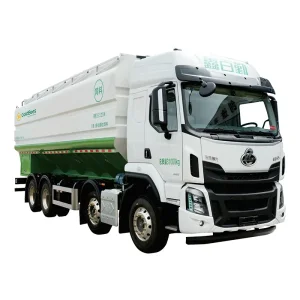
Custom China's Top Suppliers of Electric/Hydraulic Auger Bulk Feed Transport Truck - Innovative Factory Solution Manufacturers, Factory
View Specifications
CE Certification China GoldBees Livestock Transport Semi-Trailer: Smart Safety Solution by Leading Suppliers and Factory Manufacturer, Factories
View Specifications
ODM China Suppliers Day-Old Chick Transport Truck from Factory - Automated Climate Control for Poultry Logistics Manufacturers, Factories
View Specifications