Precision harvesting robotics, biomechanical bird collection, and end-to-end biosecure poultry transport logistics engineered by Xinbaiqin Special Vehicle (CP M&E Group).
Explore our flagship smart livestock, feed, and harvesting equipment line engineered for extreme biosecurity, minimal mortality, and zero-downtime agricultural operations.



Analyzing the macro-economic forces, regulatory shifts, and yield loss mitigation strategies driving global poultry integrators from manual harvesting to smart mechanical harvesting platforms.
Manual catching is consistently ranked among the most physically grueling, hazardous, and high-turnover jobs in agricultural production. Tightening labor pools in the Americas, Europe, and East Asia have elevated operational risks, driving multinational integrators to adopt self-propelled catching robots that run 24/7 with minimal operator supervision.
Rough manual handling causes wing fractures, subdermal hemorrhages, and muscular hematomas. In high-speed processing abattoirs, bird degradation directly translates into down-grading penalties. Intelligent catching mechanisms maintain controlled mechanical velocity, reducing bird bruising rates to below 1.2%.
Third-party catching crews moving from farm to farm present massive epidemiological vectors for Avian Influenza (HPAI) and Salmonella cross-contamination. Dedicated on-farm or fleet-sterilized automated harvesters with wash-down IP69K electrical systems minimize human pathogen introduction into sterile barn environments.
A granular look into the mechanical kinematics, gentle rotary pick-up fingers, adjustable transfer conveyors, and smart crate-loading interfaces manufactured by Xinbaiqin.
Our harvesters deploy high-elasticity, FDA-compliant food-grade polyurethane rotary fingers. Synchronized counter-rotating cylinders gently guide broilers toward the main transfer apron without compressing their bone structures, eliminating wing flap panic and suffocating pile-ups.
Constructed with perforated food-grade polymer belts, our multi-stage inclined conveyance system gently transports poultry under variable incline angles. Perforations clear dry litter and fecal dust, maintaining sanitary transfer while soft side guides protect delicate bird wings from entanglement.
Integrated dynamic load-cell platforms monitor bird accumulation in real-time. Automated hydraulic indexing systems dock standard modular crates, evenly distributing broilers to legal density thresholds before sealing and queuing containers for forklift extraction.
Engineered for indoor closed-barn operation, harvesters operate on dual electro-hydraulic or Tier 4 Final ultra-quiet diesel units. Variable-track rubber crawler undercarriages ensure balanced ground pressure across soft, thick floor bedding without stirring up deep dust.
Direct comparative performance metrics evaluated across commercial broiler houses operating at 40,000 birds per barn batch cycle.
| Performance Vector | Traditional Manual Catch Crews | First-Gen Mechanical Catchers | GoldBees Intelligent Harvesters |
|---|---|---|---|
| Catch Velocity (Birds/Hour) | 1,200 – 1,800 (Crew of 8) | 4,000 – 5,500 | 8,000 – 10,000 (Crew of 2) |
| Bruising & Hemorrhage Rate | 3.5% – 6.0% | 2.2% – 3.0% | < 1.2% |
| Dead on Arrival (DOA) Index | 0.35% – 0.60% | 0.25% – 0.35% | < 0.15% |
| Sanitation & Biosecurity Rating | High Human Pathogen Risk | Partial Washdown (IP54) | Hermetic IP69K Chemical Wash |
| Bird Welfare (NCC / EFSA) | Frequent Non-Compliance Violations | Moderate Compliance | Certified Animal Welfare Compliant |
| Operational Running Cost | High Volatility (Labor Shortages) | Moderate Maintenance Overheads | Optimized TCO (Electric / Hybrid) |
Equipment design is the primary barrier preventing cross-barn epidemic transmission. GoldBees platforms adhere to the strictest global farm-gate biosecurity mandates.
Every electrical harness, servomotor, laser sensor, and hydraulic solenoid is encapsulated within military-grade IP69K waterproof enclosures. Harvester units survive direct, high-pressure, caustic alkaline and acid chemical washdowns at temperatures up to 80°C.
Eliminating flat horizontal ledge pooling, all chassis weldments feature tubular or 45-degree angle geometries. Structural members are constructed from hot-dip galvanized marine-grade steel or electropolished austenitic stainless steel, completely eliminating corrosion crevices where pathogens thrive.
Key conveyance belts and gentle catching rotor fingers feature tool-less quick-release pins. This allows operational crews to completely break down, steam-clean, and disinfect high-contact mechanical components within 45 minutes between distinct farm deployments.
How GoldBees intelligent catching machines facilitate full compliance with the European Food Safety Authority (EFSA), US National Chicken Council (NCC), and global corporate ESG requirements.
Poultry harvested manually experience high cortisol surges due to inverted leg-shackling and rough handling. Low-profile harvesting tables ingest birds in their natural upright posture under low-lux blue or monochromatic lighting, lowering metabolic stress, body temperature spikes, and muscle depletion.
Global supermarket buyers require rigorous crate loading records. GoldBees automated crate loaders continuously record environmental temperature, relative humidity, bird count, and total gross crate weight, uploading cryptographic proof of animal density compliance directly to enterprise ERPs.
Eliminating dust inhalation, musculoskeletal strain, and acute eye infections associated with manual night catching, automated harvesters reposition operators inside ergonomic, climate-controlled cabins or enable complete standoff control via wireless industrial pendant remotes.
From assisted hydrostatic operation to complete SLAM LiDAR autonomous harvesting across dense multi-tier mega-houses.
Equipped with thermal imaging arrays and low-light ToF (Time-of-Flight) cameras, our upcoming guidance suites recognize bird density contours and floor obstructions, automatically calculating harvest speeds to avoid bird piling near house sidewalls.
Eliminating the need for physical guidance cables or in-floor magnetic tracks, high-precision solid-state LiDAR sensors map the internal geometry of poultry houses, dynamically maneuvering around structural support columns, feeding winches, and drinker lines.
Every GoldBees unit features 4G/5G remote industrial IoT telemetry. Critical metrics—hydraulic oil temperature, drive motor torque, vibration harmonic signatures, and belt degradation—are streamed to our factory engineering hub, flagging wear before failure occurs.
Harvesting efficiency is useless if transit logistics fail. Xinbaiqin builds specialized climate-controlled transport vehicles that interface directly with our catching technology.
Equipped with fresh-air ventilation fans, integrated evaporative cooling pads, and thermal insulation bodies, GoldBees broiler trucks guarantee that birds harvested by intelligent machinery maintain baseline body temperatures during long-distance highway hauls.
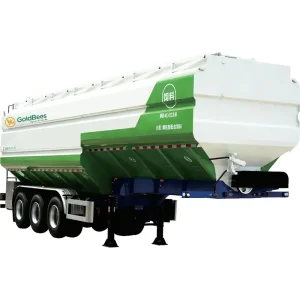
Our electric and hydraulic auger feed semi-trailers prevent feed separation and contamination. Designed with sealed individual hoppers, these transporters protect feed pellet integrity from the mill to automated on-farm feed silos.
As part of CP M&E (Charoen Pokphand Group), Xinbaiqin delivers unified industrial solutions—combining housing equipment, specialized logistics transport, and robotic field harvesters into a single integrated procurement ecosystem.
Comprehensive technical and commercial answers for agricultural engineering teams, farm managers, and fleet procurement executives.
The machine uses variable-durometer, counter-rotating food-grade polyurethane fingers that gently sweep broilers onto the ingestion table. The rotational speed matches the machine's crawler ground speed precisely, preventing birds from being trapped, pulled violently, or struck with impact force.
Yes. The chassis uses wide, high-flotation rubber crawler tracks that exert less than 0.28 kg/cm² ground pressure. This guarantees high traction across compacted, dusty, or high-moisture litter without sinking or spinning out.
A standard setup requires only 2 to 3 workers: one machine operator controlling harvester steering and ingestion speed via remote pendant or cabin, and one or two forklift operators managing full and empty crate logistics.
Under optimal barn conditions, harvesting capacity ranges between 8,000 and 10,000 commercial broilers (average weight 1.8 to 2.8 kg) per hour, significantly outperforming manual catching crews while maintaining superior animal welfare.
The entire structural body, electrical harness, and mechanical drive system are IP69K sealed. They are fully compatible with high-pressure water washing up to 80°C and industrial quaternary ammonium compounds, chlorine dioxide, and peracetic acid disinfection agents.
Yes. Leveraging CP M&E's worldwide distribution and service network, we provide factory-certified installation engineers, on-site operator training, digital parts catalogs, and regional spare parts hubs across Asia, Europe, and the Americas.
Our engineering division custom-fabricates the crate docking, handling, and loading stage to integrate seamlessly with all standard European, American, or proprietary multi-tier poultry crating systems.
Complete your supply chain with our factory-direct bulk feed semi-trailers, day-old chick transporters, and intelligent climate-controlled vehicles.