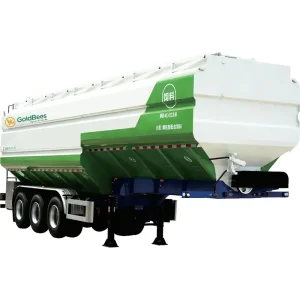
Explore precision-engineered vehicles, harvesting automations, and turnkey cold chain equipment designed under strict CE directives and ISO 9001 quality systems.

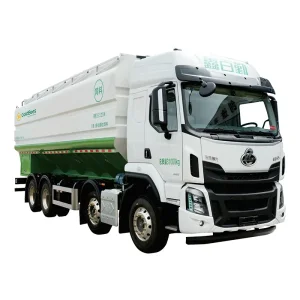
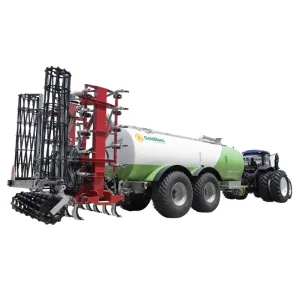
Raw milk is among the most biologically sensitive fluids moved across modern food supply chains. Maintaining total bacterial count (TBC) below strict thresholds demands precision thermodynamics and certified pressure vessel designs.
Upon extraction from the cow at approximately 37°C, fresh milk must be pre-cooled within on-farm chilling vats to 4°C within two hours to inhibit psychrotrophic bacterial growth. When transferred to mobile transport tankers, the strict international ATP agreement and standard CE hygiene protocols require the internal fluid temperature to fluctuate by no more than 1°C to 2°C over a 24-hour transit cycle without active refrigeration.
Meeting these rigorous mandates requires advanced vacuum or dense polyurethane (PU) insulated multi-compartment vessels. Modern milk tankers feature internal SUS304 or medical-grade SUS316L stainless steel linings polished to an electrolytic surface roughness of Ra ≤ 0.4 μm, preventing protein biofilm adherence and facilitating 100% sterile Clean-In-Place (CIP) sanitization cycles.
"In raw bulk milk logistics, every fraction of a degree in thermal drift directly correlates to exponential lactic acid formation and enzymic deterioration. For international dairy conglomerates, investing in CE-certified, precision-welded transport tanks is not merely an equipment upgrade; it is the ultimate risk mitigation against cross-contamination, milk souring, and batch rejection at the pasteurization plant gate."
The convergence of automated longitudinal plasma arc welding, heavy robotic dishing presses, and localized specialty chassis partnerships creates unmatched value for global fleet operators.
Xinbaiqin integrates computerized seam trackers and automated dual-torch longitudinal submerged/plasma arc welders. This guarantees uniform weld penetration, eliminates pinhole oxidation, and ensures internal seams meet radiographic inspection Class I standards without human error.
Our 66,667 m² Cixi manufacturing campus utilizes temperature-controlled, pressurized injection fixtures that inject 100mm ultra-fine polyurethane foam without air cavities. The structural cohesion binds inner and outer shells into a lightweight, high-torsion monocoque body.
By bypassing export intermediaries, CP M&E GoldBees offers direct commercial fleet builders 30% to 45% savings against European bodybuilders without sacrificing component quality, incorporating BPW axles, JOST landing gear, and Wabco ABS/EBS braking systems.
Milk harvesting terrains range from high-heat desert operations to corrugated rural arterial tracks. Our engineering teams match chassis suspension, baffle layout, and pump configurations to distinct operating zones.
Compact 8,000L to 15,000L multi-stop rigid trucks equipped with automated hydraulic hose reels, electromagnetic flow meters, and on-board sample chilling compartments designed for tight rural unpaved access roads.
Heavy-duty tri-axle 30,000L to 38,000L isothermal semi-trailers configured with 3 to 5 isolated compartments, allowing simultaneous transportation of specialized batches such as organic, Jersey A2, and standardized raw milk.
Enhanced outer shells featuring high-reflectivity mirror stainless steel, secondary solar-deflection roofing wraps, and oversized 120mm expanded polyurethane insulation capable of enduring +50°C ambient temperatures in MENA and LatAm.
Permanently mounted high-flow 360° rotary spray balls connected to a dedicated pneumatic bottom drainage valve, enabling rapid connection to automated station wash-down manifolds without entering the confined tank space.
The convergence of telemetry, electrification, and international traceability standards is defining the next generation of fresh milk transport vehicles.
Modern CE-certified tankers feature built-in multi-channel RTD temperature probes and micro-sampling pH sensors connected to GPS telemetry. Integrators receive automated alarms if temperatures rise above 6°C or if premature acidification points to bacterial fermentation in transit.
Eliminating diesel auxiliary engines, GoldBees equips milk tankers with dedicated 48V/380V lithium battery systems. These power sanitary positive-displacement lobe pumps quietly at farm collection stations, drastically reducing emissions, fuel consumption, and site noise pollution.
By shifting to advanced duplex stainless steels (such as 2205) and high-strength aluminum outer framing, tare weight is reduced by up to 1,200 kg per semi-trailer. This converts structural weight directly into legal milk payload, maximizing freight margins per trip.
Procuring fresh milk transport fleets requires balancing structural chassis integrity, pressurized vessel safety, and hygienic food contact certifications.
Importing into European or strict global jurisdictions requires verifiable CE documentation covering:
Corporate procurement officers must demand third-party metallurgical certificates confirming steel origin, non-destructive radiographic weld test reports, and factory hydrostatic pressure test results before containerized dispatch or Ro-Ro shipment.
Furthermore, ensure that the running gear configuration matches local gross vehicle weight (GVW) regulations, axle load limits, kingpin sizes (2" vs 3.5"), and dual-line EBS pneumatic connection schemas prevalent in the importing territory.
Critical considerations regarding insulation life, sanitization compliance, chassis integration, and global export handling.
For operations adhering to ATP certified standards, a minimum of 80mm to 100mm of high-density (38-42 kg/m³) rigid polyurethane foam is mandatory. This ensures an overall thermal heat transfer coefficient (K-value) below 0.35 W/m²·K, preventing thermal jumps exceeding 1°C over a typical 24-hour collection route.
Yes. While we supply complete tractor-trailer rigs and complete cab-chassis vehicles based on renowned heavy-duty brands (e.g., Sinotruk, FAW, Shacman, or Dongfeng), we also engineer unmounted tank bodies with universal subframe brackets compatible with European chassis (Scania, Volvo, MAN, Mercedes-Benz).
Each compartment features independent, sanitary stainless steel rotary spray balls operating at 2.5 to 3.5 bar fluid pressure. The curved dish heads and 1.5% sloped tank floors eliminate dead pockets, ensuring zero chemical or microbial residue remain after an alkaline-acid automated CIP wash sequence.
Our tankers incorporate dished, flanged sanitary surge baffles positioned every 2,500mm to 3,000mm. These baffles reduce dynamic liquid inertia during braking and cornering by over 60%, significantly improving driving safety while maintaining removable manhole access for visual hygienic inspections.
Review additional industry-leading bulk feed delivery trailers, biosecure poultry logistics vehicles, and advanced temperature-controlled refrigerated units.