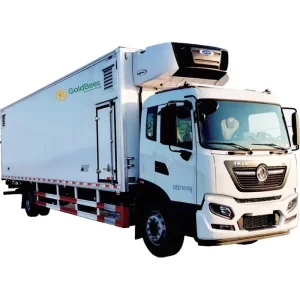
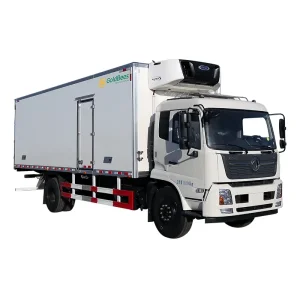
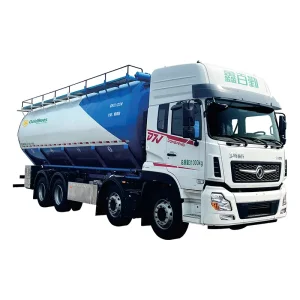
Engineered for precision farming, high biosecurity compliance, and minimal cargo mortality across industrial supply chains.
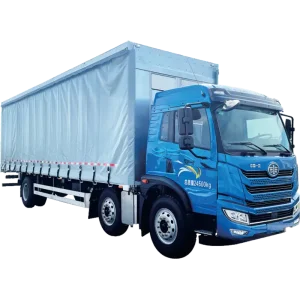
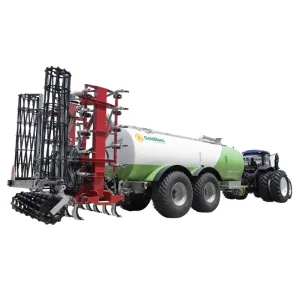


In modern high-density poultry agribusiness, the boundary between fixed farming assets and dynamic logistics infrastructure has permanently dissolved. As integrated poultry producers face escalating pressures surrounding biosecurity integrity, rising grain and feed prices, strict animal welfare compliance, and total lifecycle carbon tracking, equipment procurement can no longer be approached through disconnected, off-the-shelf catalog purchasing. Sourcing poultry machinery directly from qualified Chinese engineering manufacturers—such as Xinbaiqin Special Vehicle Co., Ltd. (operating under the GoldBees commercial brand in technical synergy with CP M&E of Charoen Pokphand Group)—represents an architectural pivot from fragmented suppliers to vertically integrated industrial equipment partners.
Industrial chicken operations lose significant annual revenue through three preventable vectors: sub-clinical thermal stress during chick and broiler transit, pellet degradation and segregation during bulk feed distribution, and biological cross-contamination caused by improper washdown designs in mechanical assemblies. Addressing these structural inefficiencies requires precision engineering across chassis layouts, aerospace-grade thermal insulation, and programmable automated multi-zone microclimate control.
GoldBees manufactures purpose-built machinery addressing every critical intervention node in the modern poultry supply pipeline.
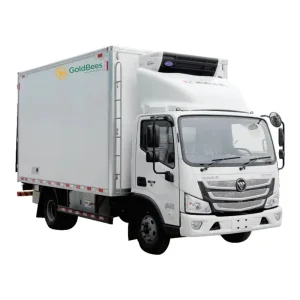
Equipped with computerized positive-pressure HVAC units, independent HEPA air filtration arrays, and multi-sensor thermal equilibrium systems that prevent cold shock and carbon dioxide build-up during long-haul transfers.
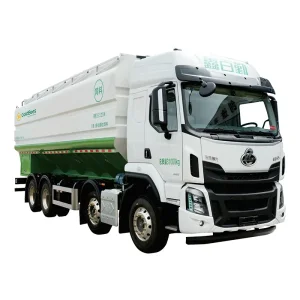
Dual-drive discharge mechanisms offering both hydraulic auger screw conveyors and low-shear pneumatic blowers. Designed with lightweight high-strength alloys to maximize payload while avoiding mechanical segregation of micro-nutrients.
Fabricated with high-grade anti-corrosive aluminum superstructures, hydraulic lift gates, integrated misting and watering ports, and natural-draft fluid aerodynamic profiles that eliminate mortality hotspots during live bird haulage.
Operating from our 66,667-square-meter modern production base in Cixi, Zhejiang, we provide international agribusiness integrators with an unyielding manufacturing buffer.
As a key manufacturing unit aligned with CP M&E (Charoen Pokphand Group), our product designs are real-world validated across thousands of operating production units globally, not confined to simulation labs.
Equipped with 30,000-watt automated fiber laser cutting tables, CNC heavy plate hydraulic bending, and robotic seam welders guaranteeing airtight, pathogen-resistant structural assemblies.
Superstructures seamlessly adapt to global commercial truck chassis including Mercedes-Benz Actros, Volvo FH, Scania, MAN, Isuzu, Hino, Sinotruk HOWO, FAW, Shacman, and Foton.
Unmatched component availability and centralized raw material inventories slash production lead times down to 25–40 days for custom fleets, compared to 9–14 months for Western European makers.
Poultry machinery must withstand hostile climatic extremes and severe infrastructure challenges. GoldBees builds custom configurations for varying regional operating parameters.
Extreme Heat & Arid Dust Proofing: Dual heavy-duty refrigeration units engineered with condenser sand-storm bypass filters, thermal body insulation thickness increased to 100mm polyurethane, and high-pressure evaporative mist cooling systems maintaining comfortable internal temps even when ambient temperatures reach +52°C.
High Relative Humidity & Monsoon Resistance: Anti-condensation dynamic internal airflow prevents moisture drops onto day-old chick feathers. Full 304/316 stainless steel hardware, electrophoretic chassis anti-rust treatments, and IP67 waterproof wiring withstand 100% relative humidity and torrential downpours.
Sub-Zero Arctic Winter Heating: Independent Webasto diesel-fired pre-heaters, insulated floor decks with liquid glycol warming circuits, and automated louvered ventilation covers ensure high-value day-old breeder flocks remain healthy across -35°C blizzard conditions.
How next-generation digitalization, electrification, and autonomous bio-monitoring are revolutionizing industrial poultry operations.
Real-time cloud monitoring of CO2, NH3, temperature, humidity, and door-opening security hashes logged to tamper-proof ERPs for full farm-to-table traceability.
Integration of high-density LFP battery architectures into medium and heavy bulk feed trucks, slashing depot-to-farm operating costs by up to 58% while eliminating farmyard carbon emissions.
Deployment of automated intelligent broiler catching vehicles that smoothly transfer 8,000 birds per hour directly into transport modules without manual handling bruises or stress.
Robotic chassis and superstructure wash bays executing multi-stage detergent foaming, 85°C high-pressure rinse, and UV-C / chemical mist disinfection in under 12 minutes.
International operations require total mechanical dependability and bulletproof biosecurity barriers.
Every GoldBees vehicle features flush interior weld lines, smooth hygienic radii, and sealed conduit tracks tested to resist 150-bar alkaline chemical cleaning cycles at 85°C without electrical faulting or rust formation.
Manufactured under strict ISO 9001, ISO 14001, and CE certifications. Electrical architectures feature dual 12V/24V step-converters, Deutsch industrial connectors, and full ADR transport compliance for European and global highways.
Supported by CP M&E's worldwide maintenance supply depots. We maintain an international 72-hour air dispatch protocol for mission-critical hydraulic valves, controllers, and HVAC motors.
Targeting critical technical parameters, biosecurity measures, custom build configurations, and international logistics execution.
Explore our full spectrum of specialized livestock carriers, intelligent pneumatic delivery trucks, and turn-key feed mill infrastructure.