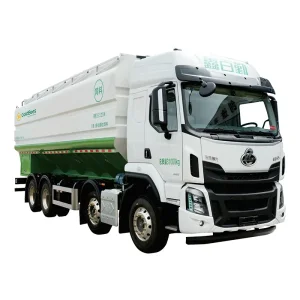
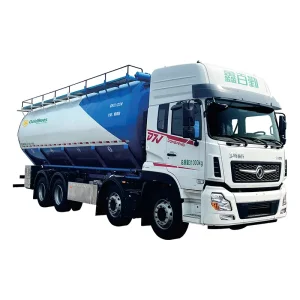
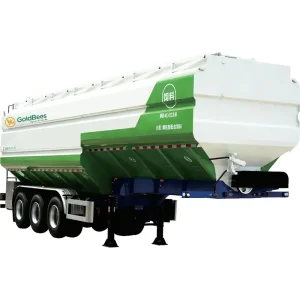
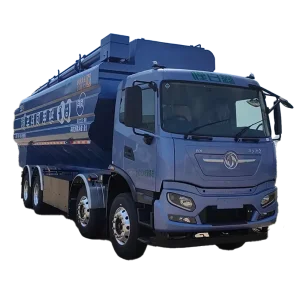
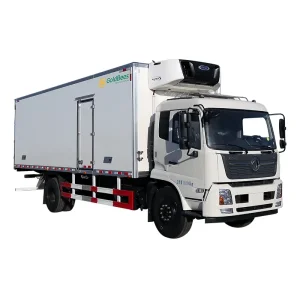
Precision-manufactured commercial transport platforms engineered for livestock biosecurity, high-efficiency bulk feed auger dispatch, and zero-compromise pharmaceutical & fresh protein cold chain preservation.
As perishable trade volumes compound under strict World Health Organization GDP (Good Distribution Practice) and HACCP sanitation mandates, modern refrigerated vehicle manufacturing has evolved from simple thermal insulation to closed-loop digital thermodynamic management systems.
Moving beyond legacy expanded polystyrene (EPS), modern factory lines utilize continuous high-pressure polyurethane (PU) injection and extruded polystyrene (XPS) sandwich panels clad in food-grade fiber-reinforced polymer (FRP). This architecture guarantees an overall heat transmission coefficient (K-value) below 0.35 W/m²·K, substantially exceeding UN ATP Class FRC benchmarks.
Cross-contamination mitigation in animal protein, livestock, and day-old poultry logistics requires active cabin positive pressure systems, UV-C germicidal sterilization ductwork, and hermetically sealed electrical conduits engineered to endure 120-bar hot caustic chemical washdowns without dielectric breakdown.
Modern fleet operators require multi-temperature flexibility. Partitioned longitudinal bulkheads allow simultaneous transport of -22°C frozen carcass cuts and +4°C chilled dairy. Real-time CAN-bus telematics upload interior humidity, ambient Delta-T, and automated defrost intervals to cloud dashboard portals.
Operating from our modern agricultural and special automotive industrial campus in Cixi, Zhejiang, Xinbaiqin Special Vehicle (associated with CP M&E) integrates end-to-end tooling, CNC laser metal forming, and automated vacuum sandwich lamination. This vertically integrated manufacturing eliminates third-party component bottlenecks and ensures complete traceability across every chassis and refrigerated box structure.
Every GoldBees refrigerated vehicle undergoes rigorous thermodynamic chamber stress testing prior to bill-of-lading issuance:
Direct factory parameters engineered to assist international corporate fleet directors, municipal planners, and cold-chain integrators in equipment tender scoping.
| Vehicle Classification | Typical Volume (m³) | Payload Capacity (kg) | Wall Structure Thickness | Thermal Unit Integration | Primary Target Applications |
|---|---|---|---|---|---|
| Light Urban Delivery Van / Box | 12 – 22 m³ | 1,500 – 3,500 kg | 80 mm High-Density PU | Direct-Drive Engine / 100% Electric ePTO | Last-mile pharma, fresh dairy, city bakery, catering logistics |
| Medium Rigid Reefer Truck | 25 – 45 m³ | 5,000 – 12,000 kg | 85 – 100 mm XPS/PU Clad | Underslung Diesel / Dual Evaporator Split | Inter-city frozen meat distribution, wholesale produce, vaccines |
| Heavy Tri-Axle Semi-Trailer | 70 – 92 m³ | 22,000 – 32,000 kg | 105 mm High-Spec Thermal Foam | Independent Diesel Genset (Carrier/Thermo King) | Trans-continental trunk haulage, primary processing plant distribution |
| Intelligent Bio-Livestock Van | 40 – 65 m³ | 8,000 – 18,000 kg | Insulated Double-Skin Aluminum | Multi-Zone Fresh Air Forced Inversion & Water Heaters | High-health breeding pigs, day-old chicks, parent stock layers |
Refrigerated vehicles engineered in China must excel across a diverse spectrum of geography, from equatorial desert heat to sub-polar tundra. Our localized engineering addresses specific global operating conditions.
Designed for operations where temperatures exceed +45°C with 90% relative humidity. Features high-reflectance gel-coats, solar radiation reflective roof layers, and tropicalized condensers prevent high-pressure compressor cutouts.
For sub-zero winter corridors down to -35°C. Systems incorporate reverse-cycle heat pump refrigeration, auxiliary fuel heating modules, insulated air-intake baffles, and heated pneumatic brake lines to prevent freezing.
Tailored for European CE cities with strict LEZ/ULEZ rules. Battery electric vehicle (BEV) chassis integration with whisper-quiet PIEK-compliant refrigeration units under 60 dBA and regenerative braking energy recovery.
Built for mountain highway passes and remote agro-pastoral hubs. Reinforced high-tensile steel sub-frames, heavy-duty mechanical leaf or adaptive air suspension, and turbocharged generator sets preserve stable refrigeration at 3,000+ meters.
Traditional refrigerated vehicles consume 15% to 25% of their total engine fuel merely driving mechanical refrigeration compressors. Our factory leads the green transition through three core technological pillars:
In commercial road transport, every kilogram trimmed from the body tare weight converts directly into legal payload and freight revenue. By adopting aerospace-grade composite core laminates, GoldBees reefer bodies achieve a 18% tare weight reduction compared to legacy sheet-metal vans.
Furthermore, 3D CFD aerodynamically profiled front radiuses and integrated side skirts reduce drag coefficients (Cd) by 11.4%, generating an estimated 2.8-liter fuel savings per 100 kilometers on highway trunk routes.
Engineering clarifications, customization options, and export certification details for commercial vehicle procurement teams.
Explore our complete range of specialized equipment including high-volume pneumatic feed dispatchers, multi-deck live poultry harvesters, and high-cube refrigerated semi-trailers.