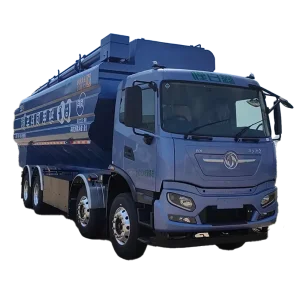
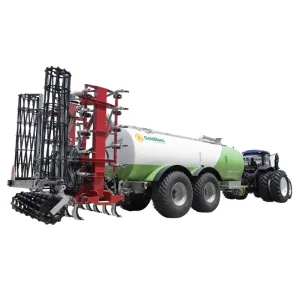
Engineered to mitigate thermodynamic losses, pathogen transference, and biological operational stress across mission-critical perishable corridors.
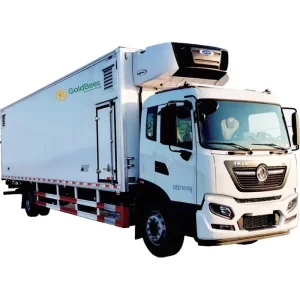
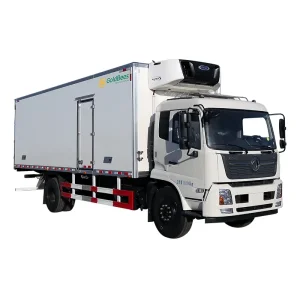



Global cold chain logistics is undergoing an unprecedented structural transition. The modern perishable cargo sector—spanning fresh agricultural yield, ready-to-cook livestock cuts, biosecure hatchery operations, and dairy production—no longer relies simply on passive insulated bodies. Modern fleet procurement mandates unbroken cold-chain intelligence, biosecurity mitigation, and real-time environmental adaptability.
Historically, transit perishability suffered from high spoilage coefficients due to manual temperature monitoring, cold-bridge leakages in body seams, and severe micro-vibration bruising. Today, international food distributors operate within tightly regulated frameworks such as FSMA (Food Safety Modernization Act), ATP (Agreement on the International Carriage of Perishable Foodstuffs), and global HACCP mandates. Fresh food transport vehicles have thus evolved from basic mechanical refrigeration haulers into mobile bio-preservation nodes equipped with active airflow distribution, IoT-monitored microclimates, and multi-temperature thermodynamic compartmentalization.
Xinbaiqin Special Vehicle Co., Ltd. (operating the specialized GoldBees commercial brand and working alongside CP M&E—the electromechanical industrial engineering division of Thailand's Charoen Pokphand Group) occupies an authoritative position within this transformation. Integrating over 15 years of technical pedigree, our manufacturing processes treat thermal insulation, weight reduction, bacterial resilience, and telemetry as a singular, cohesive biomechanical platform.
Multi-stage ducted airflow systems combined with zero-thermal-bridge polyurethane foam injection guarantee uniform temperature retention within ±0.5°C across all cargo tiers.
Continuous internal seamless welded alloy liner plates coupled with hydrophobic microbial barriers prevent cross-contamination across operational washing and chemical cycles.
Edge computing gateways track relative humidity, carbon dioxide concentrations, core refrigeration head metrics, and vehicle telematics with remote automated alerting.
Addressing the strict commercial, regulatory, and mechanical criteria defined by international food distribution conglomerates and fleet managers.
By pairing ultra-high-tensile structural steel chassis sub-frames with proprietary 5083/6061 aviation-grade aluminum box skins, tare weight is engineered down by up to 18%, significantly expanding legal dry and refrigerated payload capacity per route.
Global supermarket networks demand simultaneous haulage of deep-frozen meats (-18°C), fresh butchered pork (+2°C to +4°C), and delicate orchard produce (+8°C). Modular insulated partitions offer flexible multi-temperature layout setups.
Fresh meat and livestock haulage carries strict epidemic containment obligations. Wiring harnesses are sealed to IP69K liquid immersion protection, allowing high-pressure disinfectant power-washing at 80°C without electrical degradation.
Overseas fleet compatibility requires body sub-structures engineered to seamlessly mate with leading international chassis systems, including Scania, Volvo, Mercedes-Benz Actros, MAN, Isuzu, Hino, and leading domestic commercial chassis.
The production of specialized commercial vehicles requires an expansive industrial matrix. Sourcing high-integrity refrigerated vans or animal husbandry transport equipment from China provides global aggregators an unmatched combination of engineering verticality, manufacturing velocity, and structural cost balance.
At our 66,667 m² manufacturing campus located in Cixi Modern Agriculture Industrial Park, Zhejiang, Xinbaiqin operates automated production workshops equipped with computerized fiber laser cutting tables, 12-meter robotic tandem bending presses, and large-span vacuum bonding presses for composite sandwich panel curing. By keeping structural stamping, polyurethane foaming, subframe fabrication, and electrical control integration in-house, the enterprise removes third-party margin compounding while maintaining uncompromising quality oversight.
Backed by the engineering expertise of the CP M&E industrial network, our continuous feedback loop with working feed processing facilities, commercial swine nurseries, and egg layer facilities guarantees that every body modification reflects real-world operational testing. This industrial depth allows delivery timelines of 30 to 45 days for custom production orders—a timeline that traditional regional coachbuilders rarely match.
Our automated continuous vacuum panel-lamination infrastructure eliminates structural thermal gaps, delivering insulation heat-transfer values far below international ATP standards.
Direct supply partnerships for heavy industrial-grade aluminum extrusions, automotive hydraulics, and carrier refrigeration compressors mitigate international supply disruptions.
Complete product engineering compliant with ISO 9001 quality criteria and European CE safety directives, backed by extensive dynamic road vibration and hydrostatic leak trials.
Examining operational logistics parameters where customized vehicle engineering delivers verified, measurable performance advantages.
Operational Challenge: Day-old poultry possess fragile thermoregulatory capabilities. Sudden drafts, uneven air distribution, or carbon dioxide spikes cause rapid batch mortality.
Factory Solution: Enclosed GoldBees climate-controlled bodies integrate multi-sensor negative-pressure dynamic ventilation systems, auxiliary power generator redundancy, and water-heating heat exchangers, ensuring survivability rates above 99.7% over 1,500-kilometer routes.
Operational Challenge: High-density porcine transit generates dangerous ammonia concentrations and thermal fatigue, increasing the risk of transportation loss and infection spread.
Factory Solution: Multi-tiered lightweight aluminum alloy decks feature internal drinking systems, misting evaporative cooling nozzles, waste collection retention systems, and bio-security HEPA air intake filtration with dedicated air-handling monitoring.
Operational Challenge: High-performance animal nutrition formulas fracture under aggressive handling, causing pellet breakdown, nutrition loss, and silo bridging.
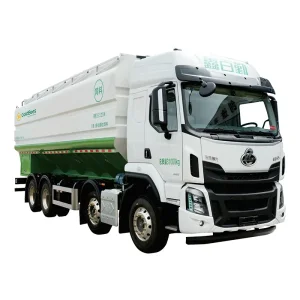
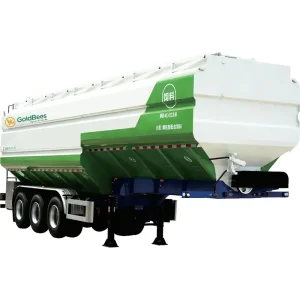
Factory Solution: GoldBees hydraulic auger conveyor semi-trailers use multi-chamber designs with hydraulic screw drives and variable-speed wireless remote controls, minimizing breakage rates below 0.3% during discharge into farm silos.
Comprehensive operational guidance for engineering teams, overseas commercial fleet buyers, and agricultural contractors.
Explore our extended catalog of animal protein logistics equipment, feed distribution bodies, and agricultural machinery.