

Direct factory engineering from Xinbaiqin Special Vehicle (CP M&E). Advanced modular designs engineered to optimize feed integrity, minimize animal transit stress, and eliminate cross-facility contamination.


How hyper-scaled animal protein integrators are reshaping procurement standards around closed-loop biosecurity, energy efficiency, and high-welfare automated handling.
The contemporary commercial poultry landscape has evolved past the limits of conventional farm structures. Modern integrators operate breeding colonies, multi-tier automated cage systems, and mega-scale feed mills that process tens of thousands of metric tons per month. In this hyper-concentrated environment, equipment failure is not an isolated mechanical delay; it represents an immediate threat to the biological security of the entire vertical chain.
According to epidemiological evaluations across major livestock belts, transport pathways—comprising bulk feed delivery trucks, day-old chick carriers, and slaughter-bound broiler haulers—represent more than 60% of pathogen transmission vectors between production nodes. Pathogens like Avian Influenza (HPAI), Salmonella enterica, and Mycoplasma gallisepticum exploit microscopic flaws: porous welds, dead angles in cargo tanks, unsealed electrical conduits, and uncleaned ventilation ducts.
In response to these operational realities, Xinbaiqin Special Vehicle Co., Ltd., functioning in strategic partnership with CP M&E (the electromechanical equipment entity of Charoen Pokphand Group), has re-engineered modern poultry logistics. By utilizing actual operating datasets from global commercial farms, our manufacturing campus bridges precision metal fabrication with microclimate HVAC, smart pneumatic discharge, and Internet-of-Things (IoT) traceability.
Fabricated using aircraft-grade aluminum alloy and robotic continuously welded seams. Smooth surfaces and internal radiused corners eliminate residue accumulation during high-pressure alkaline and acid chemical wash-downs.
Transporters for day-old chicks integrate positive-pressure HVAC units, constant temperature air jackets, and real-time CO2 scrubbing to keep chick mortality below 0.05% even across 1,000-kilometer journeys.
Our auger and pneumatic bulk feed logistics eliminate pellet pulverization. Multi-stage hydraulic pitch regulation delivers up to 60 tons per hour with a fines generation index under 0.15%.
Detailed evaluation matrices for corporate agricultural buyers: balancing capital expenditures (CAPEX), fuel economy, tare weight, and long-term chassis durability.
By shifting from standard Q235 steel to 6061-T6 aluminum alloys and high-yield BS700MC steel, GoldBees truck bodies reduce empty tare weight by 1,200 to 2,400 kg per unit. Over a standard 100,000 km annual duty cycle, this directly converts into 8-12% fuel savings when empty and higher payload capacity per run within legal axle load limits.
Frequent start-stop loading and abrasive feed dust degrade inferior hydraulic components. Xinbaiqin integrates German-engineered hydraulic drives, heavy-duty splined drive shafts, and dust-shielded gearboxes that run more than 15,000 continuous hours before overhaul.
Integrated pneumatic seal gates and precision slide-valves between compartments prevent cross-contamination between high-protein starter feeds, medicinal batches, and finisher diets, preventing costly residue transfers and protecting commercial flock integrity.
An integrated overview of our specialized engineering portfolio—from grain processing and farm feeding to humane broiler harvesting and refrigerated transport.
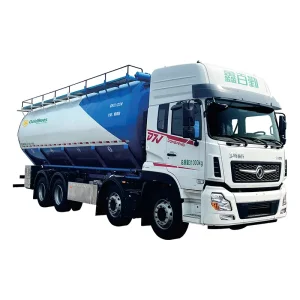
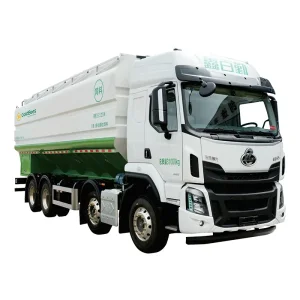
Our auger bulk feed trucks and semi-trailers move livestock feed from mill storage silos to farm elevated feed bins cleanly and efficiently. The auger system uses high-tensile alloy tubes, precision spiral flights, and variable-speed hydraulic pumps that deliver continuous conveying without crushing delicate feed pellets.
The roof auger rotates up to 180 degrees horizontally and elevates to 60 degrees, allowing clean discharge into farm silos up to 12 meters tall. For zero-emission farm operations, our dual-power models can switch from truck engine PTO to an external 380V stationary electric supply, cutting engine idle wear, emissions, and fuel costs inside farm perimeter gates.
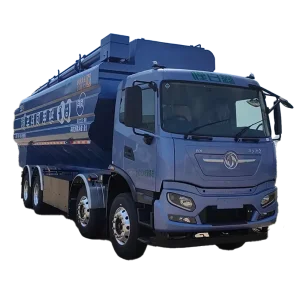
For installations with ultra-tall silos (up to 20 meters) or long pipe runs, GoldBees pneumatic discharge trucks offer completely enclosed conveying. Clean, filtered air generated by high-volume low-pressure Roots blowers moves the feed smoothly along internal delivery hoses.
Fluidized bed aeration membranes at the base of each compartment prevent bridge formation when handling sticky meals or high-fat feeds. Dust extraction fittings create a closed-loop balance between tank and farm silo, preventing fine dust releases that can carry pathogens or settle on nearby poultry houses.
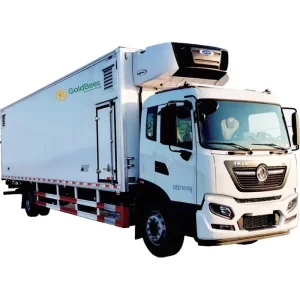
Day-old chicks cannot self-regulate body temperature; exposure to drafts, cold spots, or metabolic overheating can cause high mortality or poor lifetime performance. Our enclosed chick transporters use multi-circuit HVAC systems that maintain a uniform 32°C ± 0.5°C across the entire cargo hold.
Centrifugal blowers deliver filtered fresh air through ceiling plenums down across chick crates, sweeping away metabolic heat and CO2 before venting out base dampers. A continuous backup battery and auxiliary generator keep life-support ventilation running even if the prime mover stalls.
Manual chicken catching causes bird bruising, wing fractures, high labor costs, and elevated stress. Our intelligent chicken harvester uses soft-touch counter-rotating pickup fingers and hydraulic crawlers to gently transfer birds from litter floors to sorting conveyors and transport crates.
This automated approach harvests 5,000 to 8,000 birds per hour with a crew of just two operators. Birds are loaded into ventilated broiler transport trucks with hydraulically lifting decks, non-slip flooring, and misting systems that keep transit shrinkage under 1.2% in warm weather.
Through our direct connection to CP M&E, we supply complete turnkey feed mill systems, automated multi-tier broiler cages, automated egg collection lines, and computerized ventilation equipment. Modular design ensures smooth mechanical and digital integration between feed silos and delivery vehicle fleets.
The convergence of New Energy Vehicle (NEV) platforms, telematics, and autonomous biosecurity protocols across the GoldBees commercial vehicle line.
Integrated commercial BEV chassis with 280–420 kWh LFP battery packs, dedicated electric auger PTOs, and zero-emission delivery inside biosecure farm boundaries.
Real-time cellular transmission of in-transit metrics: chick compartment CO2 and humidity, payload weight distribution, discharge speeds, and auto-disinfection logs.
Electronic geofenced cargo locks that only open once automated thermal scanners verify the truck has completed certified perimeter washing and chemical disinfection.
Self-guided robotic chicken harvesters using LiDAR and computer vision to navigate commercial broiler houses, gently loading transport modules without human labor.
Xinbaiqin supplies tailored equipment configurations engineered to match local road regulations, climates, and biosecurity protocols worldwide.
Optimized for high heat and extreme humidity. Day-old chick and broiler trucks feature oversized condenser units, tropical-spec chillers, and corrosion-resistant coatings that hold up against salt mist and humid farm environments.
Engineered to meet strict animal welfare transport mandates (EC 1/2005). Broiler and chick bodies include continuous environmental logging, automated drinking nipples, and mechanical forced-ventilation backups.
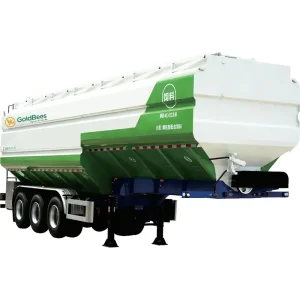
Configured for extended interstate runs and high road payload limits. Multi-axle semi-trailers offer up to 70 cubic meters of tank capacity, auxiliary air-suspension systems, and long-range diesel heating units.
Every GoldBees vehicle and feed mill module undergoes structured factory testing to verify weld integrity, electrical safety, and biosecurity performance before export.
At our 66,667 m² manufacturing complex in Cixi, Zhejiang, every vehicle moves through a strict quality protocol: ultrasonic weld testing across pressure seams, 3-hour continuous hydraulic stress tests, full-pressure tank leak testing, and extreme shower booth water-ingress inspections.
Our electrical looms undergo automated insulation and continuity testing, ensuring that control panels, sensors, and cab-mounted monitors can withstand high-pressure washdowns and caustic chemical sanitizers.
Certified compliance across all hydraulic conveyor trailers, automated harvesters, and feed mill electrical suites.
Rigid production consistency, environmental waste mitigation, and full metallurgical traceability.
Refrigerated bodies tested to international thermal insulation standards for food and perishables transport.
Direct technical answers to common questions from agribusiness buyers, fleet directors, and procurement managers.
Explore our specialized range of day-old poultry transports, multi-temperature semi-trailers, automated chicken harvesters, and bulk farm feeding solutions.

Whether you need custom chassis adaptors, multi-compartment auger trailers, or complete turnkey feed mill systems, our Cixi manufacturing team can engineer a tailored proposal for your operating requirements.