Agricultural & Life Sciences Cold-Chain Architecture

Cold Chain Transport Vehicles Company & Products in the Costa Rica Market

Engineered thermal transport solutions by GoldBees & CP M&E for Central America’s critical export corridors—bridging tropical microclimates, Pacific-to-Caribbean elevations, and stringent ATP / GDP compliance standards.

0.018

W/m·K Polyurethane Foam

-25°C ~ +15°C

Bi-Thermal Range Stability

ATP Class FRC

Certified International Standard

IoT 4G/GPS

Real-Time Cold Telemetry

Geographic & Industrial Reality

Cold-Chain Dynamics in Costa Rica: Microclimates, Corridors & Decarbonization

Operating a refrigerated fleet in Costa Rica demands superior thermal insulation and dynamic torque control far exceeding standard flatland logistics requirements.

The Dual-Ocean Mountain Challenge: Elevation and Thermal Inertia

Costa Rica presents one of the most mechanically demanding logistics landscapes in Latin America. Fleets routinely traverse from the tropical humidity of the Atlantic coastline at Puerto Limón (APM Terminals Moín) or the Pacific seaport of Caldera, scaling mountain corridors such as Route 32 through the cloud forests of Braulio Carrillo National Park, reaching altitudes over 2,000 meters before descending into the Gran Área Metropolitana (GAM). In less than three hours, external temperatures swing from 36°C with 95% relative humidity to 14°C in highland passes.

Under these conditions, standard refrigerated truck boxes suffer severe condensation penetration, rapid chassis corrosion, and severe compressor load fatigue. GoldBees vehicles overcome these localized challenges through our proprietary sandwich composite panels injected with ultra-dense, flame-retardant polyurethane foam (thermal conductivity λ ≤ 0.018 W/m·K) and vacuum-bonded under high pressure. Combined with high-grade anti-corrosive aluminum extrusion framing and double-lipped ethylene-propylene-diene monomer (EPDM) door gaskets, our superstructures prevent thermal bridging and water vapor intrusion, preserving precise temperatures without overworking the refrigeration unit.

Tropical High-Humidity Resiliency

Seamless food-grade fiberglass reinforced plastic (FRP) inner and outer skins protect against tropical mold, acid rain, and coastal salt spray along the Puntarenas and Limón coastline.

Compliance with Decarbonization Plan

Aligned with Costa Rica’s National Decarbonization Plan 2018–2050. Our NEV electric feed and cold chain chassis utilize CATL lithium iron phosphate (LFP) cells, cutting route emissions to zero.

Pharma & Life Sciences GDP Ready

Equipped for Coyol Free Zone biomedical manufacturers. Multi-point thermal mapping, redundant refrigeration circuits, and 21 CFR Part 11 compliant real-time cloud data loggers.

Engineering Parameter GoldBees / Xinbaiqin Export Specification Standard Regional Industry Baseline Operational Impact in Costa Rica
Insulation Core Material High-Density Rigid PU Foam (45-48 kg/m³) with vacuum lamination EPS or Low-Density PU Foam (32-35 kg/m³) Optimal Prevents core moisture rot under 95% coastal humidity
Thermal Conductivity (K-Factor) ≤ 0.018 W/m·K (ATP Class FRC Certified) ≥ 0.028 - 0.035 W/m·K 28% Less Fuel Reduces auxiliary reefer engine load on mountain climbs
Body Structural Framing Anodized aerospace 6061-T6 aluminum + stainless steel hardware Galvanized steel with exterior exposed fasteners Anti-Corrosion Eliminates salt-fog oxidation near Moín & Caldera ports
IoT Telematics & Monitoring Integrated 4G/GPS sensor suite, door-open alerts, multi-probe data Manual analog loggers or third-party detached trackers Audit-Proof Meets FDA & EU Good Distribution Practice (GDP) audits
Subframe Mountain Durability High-strength QSTE700TM steel, laser-welded with anti-torsion joints Standard carbon steel Q235, rigid channel welding Zero Chassis Cracks Absorbs Route 32 & Cerro de la Muerte torsional twists
Operational Scenarios

Engineered for High-Value Costa Rican Product Pipelines

How GoldBees specialized fleet platforms secure quality, maximize cold continuity, and safeguard international shipment margins across key Costa Rican economic sectors.

MD2 Golden Pineapple & Banana Export Corridors

Costa Rica is the world’s leading exporter of fresh pineapples, predominantly grown in the Huetar Norte and Atlantic regions. Post-harvest, core temperatures must drop to 7°C–10°C rapidly without cold injury or condensation accumulation that induces mold. GoldBees fresh produce transport solutions deliver engineered airflow floor ducts that guarantee uniform air circulation through palletized loads from field packhouses in San Carlos to APM Terminals Moín.

Life Sciences & Biomedical Corridors (Coyol Free Zone)

With medical devices being Costa Rica’s top merchandise export, pharmaceutical and biomedical giants require 100% GDP compliance for active components and diagnostic kits. Our high-precision multi-temperature bodies maintain validated +2°C to +8°C or deep frozen -20°C profiles with independent auxiliary power backups, automatic temperature alarm triggers, and complete tamper-evident digital trip logs.

Dairy & Fresh Beef Cold Chains (Monteverde & Guanacaste)

Transiting fresh milk, cheeses, and artisanal beef from northern farming belts across unpaved mountain switchbacks requires high-durability air-suspension chassis and sanitary stainless steel floor troughs. The hermetically welded interior flooring prevents leakage of brine or fluids, allowing complete high-pressure sanitization between routes to meet SENASA sanitary mandates.

Poultry, Hatcheries & Integrated Feed Security

Collaborating with CP M&E engineering resources, GoldBees delivers fully biosecure day-old chick transporters and pneumatic bulk feed haulers to Costa Rica’s poultry integrators. Controlled micro-environments safeguard vulnerable chicks against altitude sickness, oxygen starvation, and thermal stress during transit across the continental divide.

Integrated Manufacturing Hegemony

Advanced Production Standards: Xinbaiqin & CP M&E Global Synergy

Combining Thailand’s Charoen Pokphand Group agribusiness pedigree with high-precision Chinese automotive engineering to deliver unmatched vehicle life-cycle ROI.

Xinbaiqin Special Vehicle Co., Ltd. operates a state-of-the-art 66,667 m² manufacturing campus in Cixi, Zhejiang, producing over 2,000 specialized heavy and medium-duty units annually. In direct partnership with CP M&E—the electromechanical division of multinational agribusiness titan Charoen Pokphand Group—our product line reflects more than 15 years of end-to-end biological and cold-chain transport telemetry.

Unlike regional bodybuilders that rivet pre-formed panels together, GoldBees utilizes automated, single-shot continuous vacuum-foaming presses. This seamless structural technique eliminates mechanical fast-point thermal bridges, prevents panel delamination under extreme road vibration, and preserves panel rigidity over decades of rigorous service. Every unit exported to Central America is engineered on proven export chassis platforms or supplied as completely knocked-down (CKD) / fully built-up (CBU) bodies compatible with leading commercial chassis (Isuzu, Hino, Freightliner, Mack, Sinotruk, and FAW).

Accelerate Your Costa Rican Fleet Modernization

Connect with our bilingual technical engineering team. We supply tailored weight-distribution assessments, refrigeration thermal load calculations, and turnkey export solutions delivered to Puerto Caldera or Moín.

Send Inquiry Now - Consult Our Cold Chain Engineers
Expanded Fleet Portfolio

Complete Thermal & Specialized Agricultural Transport Line

Original GoldBees specialized fleet systems engineered for biosecure farm operations, animal transport, automated harvesting, and long-range cold transport.

Livestock Transport Costa Rica Livestock Transport Semi-trailer GoldBees

Smart Guardian Livestock Transport Semi-Trailer for Central American Ranches

Multi-deck ventilated trailer featuring filtered climate control, hydration mists, and automated loading ramps for cattle and swine safety.

Multi-Tier Decks Forced Aeration Effluent Tanks
View Product Specification
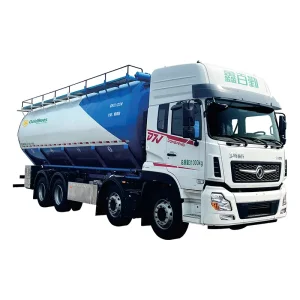
Bulk Feed Logistics Costa Rica Intelligent Pneumatic Bulk Feed Truck

Intelligent Pneumatic Bulk Feed Truck for Biosecure Silo Discharge

Enclosed pneumatic blowing delivery system safeguarding feed hygiene and nutritional integrity for high-volume dairy and poultry farms.

Dust-Free Discharge Multi-Cell Silo Zero Pellet Breakage
View Product Specification
Reefer Semi-Trailer High Quality Refrigerated Semi-Trailer Costa Rica

Heavy-Duty Refrigerated Cold-Chain Semi-Trailer for Intermodal Logistics

Industrial-grade refrigerated trailer engineered for extreme operating hours between Atlantic agricultural farms and Pacific destinations.

Heavy Payload Class FRC Insulated Dual Airflow Ducts
View Product Specification
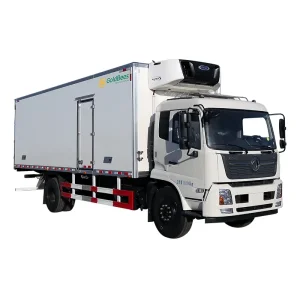
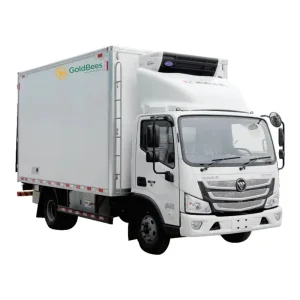
Urban Distribution Refrigerated Truck for Cargo Protection Costa Rica

Intelligent Multi-Functional Refrigerated Truck for Supermarket Supply

Precision temperature zoning for mixed fresh grocery distribution across retail networks in Heredia, Cartago, and San José.

Multi-Temperature Hydraulic Tail Lift Thermal Curtains
View Product Specification
Export Semi-Trailer GoldBees Cold Chain Semi-Trailer Innovative Solutions

High-Efficiency Long-Haul Refrigerated Semi-Trailer for Central America

Aerodynamic styling and lightweight chassis alloy profiles minimizing tare weight while expanding commercial export payload limits.

Lightweight Tare Optimized TCO Dual Spare Mounts
View Product Specification
Poultry Automation Intelligent Chicken Harvester Machine Costa Rica

Intelligent Automated Chicken Harvester for Industrial Poultry Farming

Reduces bird stress, wing damage, and catching labor overhead with gentle mechanical transfer directly into transport containers.

Animal Welfare Built High Throughput Labor Reduction
View Product Specification
NEV Clean Energy NEV Electric Bulk Feed Transport Truck Costa Rica

NEV Pure Electric Bulk Feed Transport Truck (Zero Tailpipe Emissions)

100% battery-electric heavy hauler engineered for corporate decarbonization targets, utilizing regenerative braking on downhill grades.

Zero Emissions Regen Braking CATL LFP Battery
View Product Specification
Farm Post-Harvest Fresh Produce Sorting and Transport Vehicle GoldBees

High-Efficiency Fresh Produce Mobile Sorting and Field Transport Unit

Accelerates the farm-to-shelf journey for delicate berries, mangoes, and vegetables, consolidating harvest sorting with rapid chilling.

Fast Field Chilling Sort & Stow Durable Body
View Product Specification
Technical & Procurement Intelligence

Frequently Asked Questions: Cold Chain Fleets in Costa Rica

Authoritative engineering, import compliance, and lifecycle maintenance answers for logistics directors and fleet procurement managers.

How do GoldBees refrigerated vehicle bodies resist high coastal humidity and salt-fog corrosion in Puerto Limón and Caldera?
Our superstructures employ high-grade antibacterial gel-coated fiberglass reinforced plastic (FRP) on both interior and exterior skins, sandwiching high-density closed-cell polyurethane foam. We eliminate external steel welds and exposed carbon fasteners, using anodized marine-grade aluminum alloy profiles and 304/316 stainless steel lock rods, hinges, and hardware. Subframes undergo comprehensive multi-stage cathodic electrodeposition (e-coating) and epoxy zinc priming, successfully passing 1,500-hour continuous salt spray testing under ASTM B117 protocols.
Can GoldBees bodies be mounted onto locally sourced truck chassis in Costa Rica?
Yes. We engineer customized mounting subframes that integrate seamlessly with all major truck brands operating in Central America, including Isuzu, Hino, Fuso, Freightliner, International, Mack, FAW, and Sinotruk. We can supply complete fully built-up units (CBU) or ship completely knocked-down (CKD) insulated kits with pre-wired refrigeration circuits and subframe bolt kits engineered to match your local chassis wheelbase and MOPT (Ministerio de Obras Públicas y Transportes) axle weight regulations.
What certifications do your thermal transport units hold for pharmaceutical and perishables export?
GoldBees refrigerated bodies are built in accordance with international ATP standards (Class FRC for heavily insulated multi-temperature operations). For clients in Costa Rica’s Coyol and GAM Free Trade Zones, our units are certified compliant with Good Distribution Practice (GDP) standards and FDA Title 21 CFR Part 11 requirements. This includes multi-point calibrated temperature sensor arrays, independent data recording with battery backups, door opening cycle logs, and real-time cloud-based telematics reporting via 4G/GPS.
How does the Costa Rica topography (e.g., Route 32 and Route 27) impact refrigeration unit selection?
Steep gradients and heavy traffic along routes connecting the Central Valley to coastal ports place high continuous loads on vehicle powertrains. For heavy-duty operations, GoldBees recommends independent diesel-powered refrigeration units (Thermo King, Carrier Transicold, or high-tier Chinese OEM equivalents) to maintain consistent cooling capacity regardless of truck engine RPM during long mountain climbs. Furthermore, our lower thermal conductivity (λ ≤ 0.018 W/m·K) minimizes thermal gain by up to 28% compared to regional alternatives, preventing compressor overheating in stop-and-go mountain traffic.
What is the delivery lead time and international shipping procedure to Costa Rican ports?
Standard vehicle and body production ranges from 25 to 45 business days depending on customization complexity. Sea freight from Ningbo-Zhoushan or Shanghai ports to Puerto Caldera (Pacific) or Puerto Limón / Moín (Caribbean) typically takes 22 to 32 days. Our international sales and logistics team coordinates complete documentation including commercial invoices, packing lists, Certificate of Origin (Form E or General CO for bilateral tariff reductions where applicable), and ATP inspection certificates to ensure rapid clearance through Costa Rican customs (Dirección General de Aduanas).